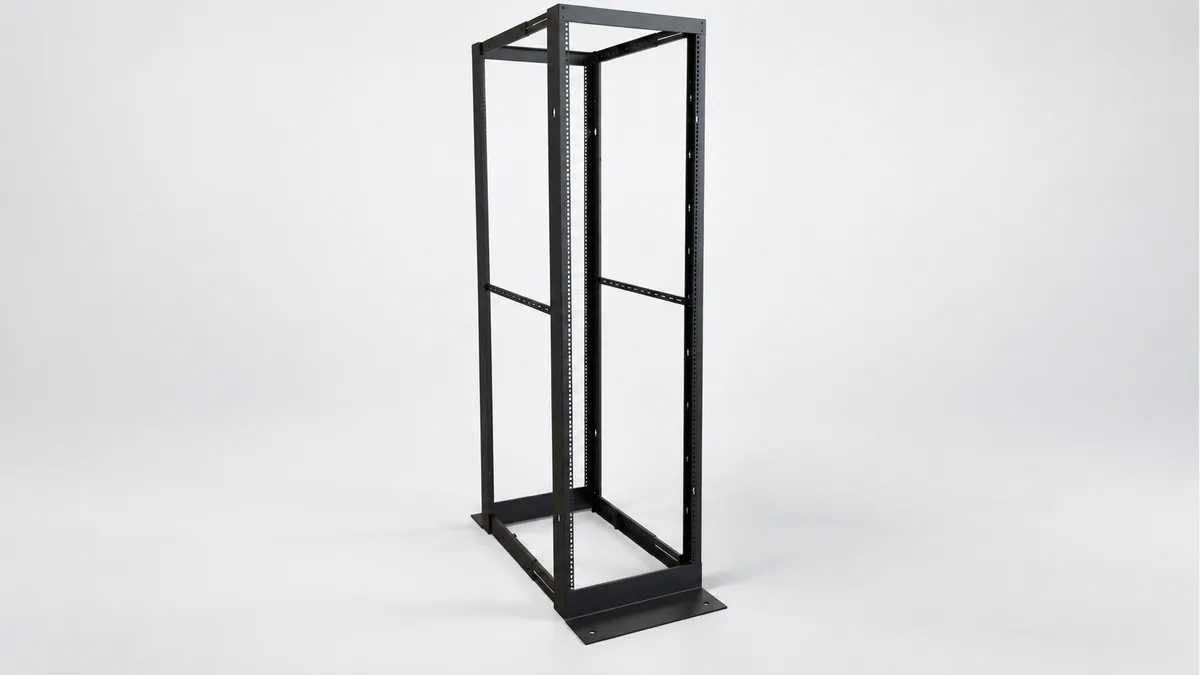
Welded Server Rack Frames to your design
Order a welded metal rack frame to carry your server or rack-mounted energy equipment. REALJET combines drawing-defined plate parts, purchased sections, welding and required interface machining for the frame you specify.
Choose the part and delivery condition
| Your order | Information that sets the scope |
|---|---|
| Welded frame | Frame drawing, section specification and weld requirements |
| Frame with machined interfaces | Rail, floor and panel datums with finished tolerances |
| Frame with listed brackets | Bracket drawings, hardware list and assembly sequence |
The supply covers the structural frame and listed attachments. Servers, batteries, power distribution and electrical assemblies are separate. OCP or other rack compatibility is claimed only for a design and acceptance scope you have specified.
Fit it to the equipment around it
Rail interfaces must stay aligned after welding and finishing. Define the rail datums, frame diagonals, base connections and panel clearances. Include the installed loading arrangement so the inspection plan addresses the frame as it will be used.
| Intended installation | Equipment interface to supply |
|---|---|
| AI equipment | AI compute rack |
| Battery storage equipment | Rack-mounted storage and energy-control equipment |
Plan the manufacturing around these features
The steps below are proposed for the drawing review. Your material, geometry and acceptance requirements determine the final route, tooling and inspection provision.
Locate the frame interfaces
Review member preparation, weld access and the rail/base datum scheme. Define which purchased sections enter the frame and how they are identified.
Review welding and restraint
Plan tack-up, connection order and restraint around the rail interfaces. Measure the frame after release from the fixture so restraint does not conceal free-state distortion.
Machine only specified interfaces
Review access for post-weld face or hole machining and the lifting arrangement. Finish protection and rail locating faces are resolved before treatment.
Manufacturing capability for your component
| Your component feature | Existing process and its use | Confirm for your order |
|---|---|---|
| Frame members and brackets | Plate preparation and welded fabrication. Prepare members and locate rail/base interfaces before selecting the joining sequence. | Purchased sections, weld access and the rack datum arrangement. |
| Welded frame assembly | FANUC robotic welding lines and fabricated subassemblies. Use the existing welded-structure experience to review fixturing and distortion control for the rack design. Robotic use depends on geometry and access. | Rack-specific fixture and free-state geometry measurement. |
| Finished mounting interfaces | Drilling, boring, tapping and machining/assembly coordination. Review which rail or base interfaces require machining after joining. | Machining envelope, lifting/handling and the required inspection reach. |
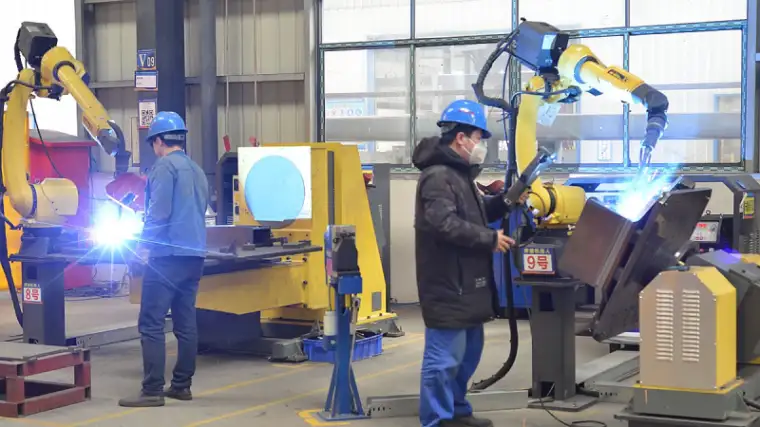
The welding workshop shows the established fabrication route. Whether this rack uses robotic or manual welding is decided from access, material and the approved joining details.
Define what the first article must demonstrate
| Feature | Proposed check | Record to agree |
|---|---|---|
| Free-state frame geometry | Measure diagonals and relevant straightness/alignment with the frame supported as specified after fixture release. Confirm equipment can cover the frame size. | Dimensions, support locations and clamped/free condition. |
| Rail and base interfaces | Measure rail mounting coordinates and base connections from the common datum; use the specified rails or gauges for a separate fit check. | Datum-based interface results and rail-fit checklist. |
| Structural test if ordered | Agree load distribution, supports, measurement positions and transport-test scope before selecting a qualified test route. | Approved test plan and report; test capability/location to be confirmed. |
Identify the drawing revision, measurement datums and pass/fail limits before the sample is made. The quote confirms the available measuring setup, any mating fixture and whether a specialist test needs an external provider.
Packing for your next assembly step
Specify the delivery condition, lifting locations and destination. Frame size and installed brackets affect packing volume; removable attachments can be reviewed if your assembly plan permits them. State the quantity and delivery city so packing volume and the requested delivery terms can be included.
Questions before you send drawings
Is a diagonal check enough to accept the rack frame?
No. Diagonals help describe squareness, but rail location, straightness and base interfaces also need checks. Measurements should identify the support condition and whether the frame is free of assembly-fixture restraint.
Can the frame be made for our rail spacing?
Yes. Provide the rail interface drawing, datum scheme and required rack envelope. Include the mating rail specification or checking fixture where available.
What should I send for the drawing review?
Send the dimensioned PDF, available STEP/DXF/DWG files and assembly view. Include material, finish, quantity, delivery city and drawing revision. Mark the features in the inspection plan that control acceptance.
Can we approve a sample before ordering repeat quantities?
Request a sample or pilot batch with the agreed dimensional report and any mating checks. Scope, timing and test provision are quoted after review; repeat supply follows the accepted drawing revision and any agreed sample changes.
Discuss your server rack welded frame
Send the part and assembly drawings with your quantity and required delivery condition. Highlight the interfaces and checks listed above that matter to your order.
Attach files in your email application. To arrange file transfer first, use the enquiry form.
AI server and data-center components → · Battery storage, EV charging and solar components →