What full span means for the line
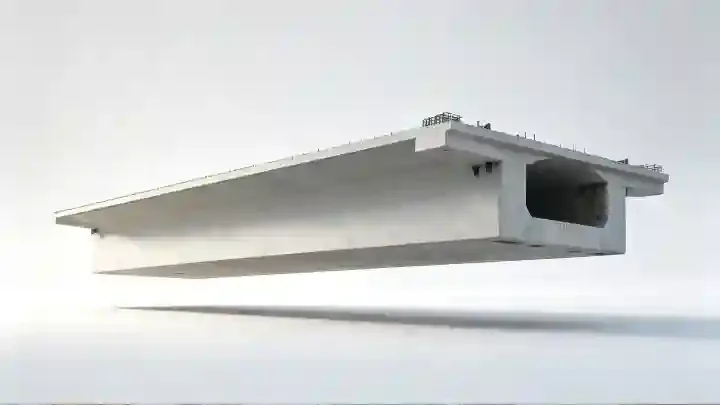
A full-span box girder is cast as one complete bridge span, at full deck width, and erected as a single unit. On high-speed rail work the common double-track unit is 32.6 m long, 12.6 m wide and about 3 m deep, with a design concrete volume close to 290 cubic metres. A yard producing these units for one contract reported 524 girders at about 820 t each, cast on seven beds with 42 double-layer storage positions in a site of 8.85 hectares (Shaoyang municipal government report).
Those figures decide the shape of the plant before any equipment is chosen. The unit cannot be turned over, an ordinary workshop crane will not lift it, and it cannot sit on the ground without a designed bearing arrangement. Handling capacity becomes the constraint that the mould, the casting bed and the yard layout all have to respect.
How it differs from segmental and in-span box girder lines
Buyers often compare three families that all produce box sections, and the differences matter more than the similarities.
| Full-span box girder | Segmental box girder | In-span box girder | |
|---|---|---|---|
| Casting unit | One complete span at full width | Short segments, later assembled | One span, often narrower section |
| Joints | Few, at span ends | Many, match cast and glued or stressed | Few, at span ends |
| Mould count | Low, but each mould is very large | High, one set per segment geometry | Moderate |
| Handling | Straddle carrier or gantry in the 900 t class | Segment-sized lifting gear | Girder-sized lifting gear |
| Geometry flexibility | Fixed per project section | High, geometry set per segment | Moderate |
| Tolerance driver | Deck width, camber and bearing positions | Match-cast joint alignment | Bearing and camber |
| Plant footprint | Long casting beds plus heavy storage | Casting hall plus match-cast area | Long beds plus storage |
A full-span line is therefore closer to a heavy civil precast yard than to a factory production line. Output is measured in girders per day, not in takt time per workstation, and the yard is sized around storage as much as around casting.
The casting bed sets the rhythm
Curing and storage, not casting, usually set the output of a full-span yard. A girder stays in its mould until it reaches transfer strength, then moves to storage where it continues to gain strength and completes its prestressing stages. Storage positions hold the unit for weeks, not hours.
The reported yard above ran a four-day mould cycle against a traditional six, with average output around 1.5 girders per day across seven beds. The arithmetic is worth doing early in planning, because it ties together three numbers that buyers often set independently: the contract quantity, the erection schedule, and the number of casting beds. If the bridge erection programme needs four girders a day and the mould cycle is four days, the line needs sixteen beds plus storage for the curing time. The bed count, more than crane capacity, is usually what makes a full-span plant expensive.
Mould: integral formwork rather than a set of panels
A full-span mould is a large hydraulic assembly with side forms, an internal form for the box void, end forms carrying the anchorage geometry, and a deck arrangement that sets the cross fall and the edge profile. On the yard cited above the moulds are described as integral hydraulic systems operated from a control panel, which is the normal direction for this component because manual setting of a 32 m form is slow and inconsistent.
Three things about the mould decide whether the line works:
- Stiffness under a single large pour. Roughly 290 cubic metres of concrete arrives in one operation, and the form pressure on the lower webs is significant. A mould that deflects will produce a girder that is out of tolerance in web thickness and in deck width.
- Repeatability of the internal form. The box void has to be centred and withdrawn without damaging the invert, and the withdrawal sequence has to suit the end forms and any diaphragms.
- Access for fixing and inspection. Cast-in items, ducts and reinforcement have to be reachable before the pour and checkable during it.
Realjet lists full-span box girder among the component families its lines can be configured for, alongside T-girder, box girder and segmental girder, on the precast concrete production line page. The mould type, operating method and number of sets are project decisions made from the approved section and the production target, not catalogue choices.
Reinforcement, ducts and cast-in items
The cage for a full-span girder is a factory-made item in its own right. It is assembled on a jig, lifted as a unit or in a small number of units, and positioned to a tolerance that keeps cover correct along the whole 32 m length. On high-speed rail work the cage includes the anchorage reinforcement around the post-tensioning ducts, and the duct positions themselves are set to a tighter tolerance than ordinary building work because the tendon profile controls the camber.
The cast-in list is longer than buyers expect on a first project: bearing plates and their anchorages, drainage sleeves and spigots, parapet or noise barrier sockets, earthing connections, inspection access, and lifting inserts. Each of these needs a fixing method in the mould that survives vibration and does not leak grout.
A pre-pour dimensional check against the approved drawing is the cheapest quality control in the plant. Grout loss around a displaced duct or a rotated bearing plate is a repair that cannot be fully undone.
Concrete, curing and two-stage prestressing
Full-span girders are usually cast in one continuous operation, so the concrete supply has to be matched to the placement rate rather than to the batch plant's nominal capacity. Placement temperature, slump and the sequence along the span all affect whether the two webs fill evenly.
Curing is handled in the mould on many modern yards, with temperature and humidity controlled rather than left to ambient conditions. The reason is the strength at transfer: prestressing is applied when the concrete reaches a specified strength, and steam or sprayed curing shortens that wait without sacrificing the early strength gain.
Prestressing on these girders is commonly split into two stages, an initial tensioning that allows the girder to be moved and a final tensioning after it has aged. The mould and the casting bed have to be arranged around that sequence, and the storage plan has to keep the girder accessible for the second stage. Duct grouting follows, and its records belong with the girder.
Lifting, storage and ground bearing
The transport and erection chain for these units runs in the 900 t class, with straddle carriers moving girders from the bed to storage and transporters running them to the erection front (report on high-speed rail girder handling). A plant planning a full-span line is planning for that equipment, its runway, and the ground beneath it.
Storage is more than a parking area for finished units. Double-layer stacking, which is normal on these yards, doubles the load on the lower girder and on the ground. Storage pedestals are set to the same bearing positions the girder will see in service, because a girder supported at the wrong points will take a set that shows up as a camber error at erection.
Two checks belong in the plan: a ground bearing assessment for the loaded storage area, and a camber measurement routine that records each girder at transfer, at final tensioning and before dispatch.
Transport and erection interface
The line's output is only useful if each girder can travel from the yard to the pier. Route surveys cover bridge clearances, turning radii, road load limits and the temporary works at the erection front. Where the route cannot take the full width, the section is revised before the mould is built, not after.
Erection itself uses a launching gantry or a bridge erection machine that picks the girder from the transporter and sets it on the bearings. The interface that catches buyers is the bearing: the girder's bearing plate positions, the bearing shelf dimensions and the survey datum all have to agree between the precast yard, the bearing supplier and the erection contractor.
What to fix in the RFQ
- The approved cross section, span set, and whether more than one section is required.
- Contract quantity, erection programme and the required daily output, stated separately from the mould cycle assumption.
- Mould type and operating method, with the number of sets and the intended casting bed arrangement.
- Tolerances on deck width, web thickness, depth, camber and bearing positions, referred to the project specification.
- Reinforcement supply and cage assembly scope, and who owns the jigs.
- Duct system, anchorage type and the prestressing stages, including the strength at transfer.
- Curing method and the target cycle time from pour to transfer.
- Lifting insert type and position, matched to the handling equipment.
- Storage arrangement, stacking height and the ground bearing assumption.
- Site conditions: available area, power, steam or heat source, and the transport route limits.
Who decides what
| Decision | Owner | Why it sits there |
|---|---|---|
| Cross section, span and camber | Designer | Follows structural design and erection method |
| Tolerances and acceptance criteria | Designer, per project specification | Sets what the mould and the yard must hold |
| Mould type and operating method | Supplier, approved by buyer | Depends on geometry, cycle and plant practice |
| Number of casting beds | Buyer, with supplier input | Tied to contract quantity and erection programme |
| Curing method and cycle | Supplier proposal, buyer approves | Affects output and energy supply |
| Handling equipment capacity | Buyer | Depends on girder weight and yard layout |
| Storage layout and ground works | Buyer, with civil designer | Site-specific and outside equipment supply |
| Route and erection method | Erection contractor | Depends on temporary works and authority limits |
Where the line order starts
A full-span box girder line is planned backwards from the erection programme. The programme sets the daily output, the output sets the bed count and storage, storage and weight set the handling equipment, and all of it lands on the mould as a tolerance and stiffness requirement. Buyers who start with the mould usually end up revising the yard.
Realjet supplies production lines for precast concrete components rather than the girders themselves, covering line planning, equipment, installation and commissioning within the agreed scope. The production line page sets out the component families and configurations, and it is the right place to start a project brief with the span set, quantity and site constraints attached.