
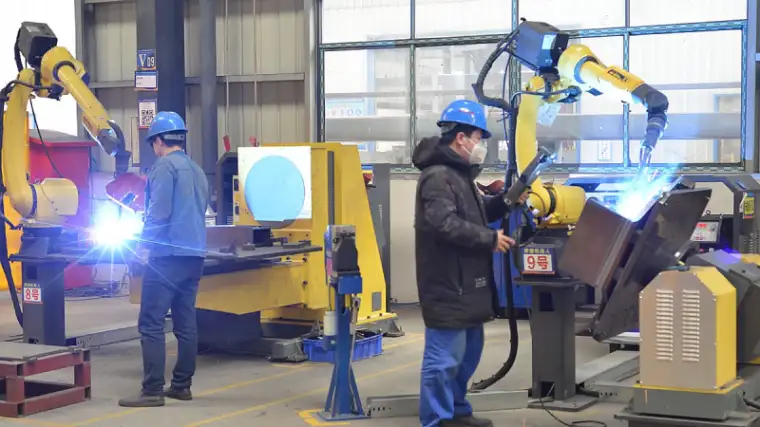
Start the RFQ with the finished assembly
A welded machinery frame may look simple on a general arrangement drawing, yet the purchasing scope can include plate preparation, formed parts, welding, stress-control measures, interface machining, coating, assembly and inspection. If bidders make different assumptions about those operations, their quotations will not be comparable.
Begin with the function of the finished frame. State what it supports, how it connects to the rest of the machine, which loads and interfaces govern the design, and whether Realjet is being asked to manufacture to released drawings or to participate in a design review. Keep design authority explicit. A contract manufacturer should not quietly fill gaps that belong to the equipment designer.
For a useful quotation from a custom machinery component manufacturing supplier, send the complete assembly context rather than isolated part drawings. Include the general arrangement, detail drawings, bill of materials, 3D model when available, revision status and the expected batch or annual quantity.
Define the drawing hierarchy and revision status
The RFQ should state which document controls when the 2D drawing, 3D model and bill of materials differ. It should also identify released files, reference-only files and information that remains provisional. Without that hierarchy, one bidder may price the current revision while another adds contingency for likely changes.
For each drawing, define:
- drawing number, title and revision;
- material grade and applicable material specification;
- dimensions and tolerances that control fit or function;
- weld symbols, weld size and inspection requirements;
- machined surfaces, datum scheme and surface-finish requirements;
- coating system and areas that must remain uncoated;
- purchased components and whether the buyer or supplier provides them; and
- required identification and traceability marks.
ISO 2553:2019 defines rules for representing welded joints on technical drawings, including information about geometry, manufacture, quality and testing. ISO 1101:2017 defines the symbol language for geometrical tolerancing. These standards do not select tolerances or weld requirements for the designer. They provide a common language once the project has chosen its specification basis.
Separate fabrication tolerances from machined interfaces
Applying one tight tolerance to the whole frame usually increases price without improving function. Large welded structures move during fit-up, welding and thermal processing. Machined mounting faces, bores and alignment features may need close control, while non-functional plate edges and access openings may accept a wider range.
Mark the functional datums first. Then identify which relationships must be achieved after welding, such as bore-to-bore position, mounting-face flatness, shaft alignment or the location of a pivot interface. Tell bidders whether those features are machined in one setup, measured after fabrication or controlled by a trial assembly.
If a dimension can only be achieved by machining after welding, say so. If machining allowance is included in the drawing, identify it clearly. This lets the supplier plan material preparation, weld sequence, fixturing and final machining around the same acceptance condition.
Make the welding quality basis quotable
Do not request "high-quality welding" without a defined basis. State the governing welding standard, material group, required procedure qualifications, welder qualifications, acceptance level and non-destructive testing scope. Identify critical joints and any restrictions on repair.
ISO 3834-2:2021 defines comprehensive quality requirements for fusion welding in workshops and at field installation sites. Citing it does not automatically define the complete job. The RFQ still needs to state the project standards, inspection responsibilities and records required for the purchased frame.
Ask each bidder to describe the planned route at quotation stage. A useful response identifies the main subassemblies, fit-up method, welding sequence, distortion-control approach, hold points and the stage at which critical interfaces are machined. The objective is not to approve a full manufacturing procedure before award. It is to expose assumptions that materially affect cost and delivery.
Specify inspection evidence before comparing price
List the evidence that must accompany delivery. Depending on the project, this may include material certificates, weld procedure and personnel qualification records, dimensional reports, non-destructive testing reports, coating records, purchased-component certificates and final release documentation.
Tie each record to an inspection point and responsible party. For example, a machined bore may require a dimensional result against a drawing characteristic, while a coating requirement may need surface-preparation and dry-film-thickness records. Avoid asking for a generic "quality dossier" because bidders may interpret that phrase very differently.
Also define access for buyer or third-party inspection. State which points require notification, witness or approval before work continues. Late inspection requirements can interrupt production and create costs that were absent from the original quotation.
Put quantity, packaging and delivery into the same scope
A prototype, a first production batch and repeat annual orders create different manufacturing plans. Give bidders the expected quantity, likely release pattern and whether tooling or fixtures should support future batches. Ask them to separate one-time engineering or tooling charges from recurring unit prices.
Packaging should reflect the finished interfaces. Machined faces, ports, threads and coating need suitable protection. State lifting points, centre-of-gravity information, transport constraints and any preservation period. If delivery is phased, define which documents and loose components travel with each assembly.
Before issuing the RFQ, check that every bidder receives the same revision set, quantity basis, inspection scope and delivery boundary. Realjet provides cutting, forming, welding, machining, coating and inspection for made-to-drawing machinery components, with the final route and responsibilities confirmed in the agreed manufacturing scope. A controlled RFQ gives both sides a clearer basis for technical review and price comparison.