In a residential frame the staircase is rarely the largest element, and it is often the one that decides whether the trades can work above the second floor. It is also the building component whose finished geometry is fixed by regulation rather than by the architect's preference, which makes it a poor candidate for improvisation and a good candidate for factory production.
A precast stair and balcony production line is a narrower proposition than a wall panel line. The components are few, the tooling is specific, and the decisions that matter are mostly about how a flight is cast and how many moulds the programme needs.
Geometry comes from the building, not the factory
Step geometry is regulated. The US workplace standard for stairways, 29 CFR 1910.25, requires standard stairs to sit at 30 to 50 degrees from horizontal, with a maximum riser of 9.5 inches (24 cm), a minimum tread depth of 9.5 inches (24 cm) and uniform riser heights and tread depths between landings. National building codes set their own numbers, and most of them land in the same region.
Once the floor to floor height, the available stair core and the local code are fixed, the riser and going are fixed too, often to within a few millimetres. A producer who buys a mould with fixed steps has bought a mould for one floor height. A producer whose projects vary between 2.8 m and 3.2 m storey heights has bought several.
The European product standard for the component is EN 14843, precast concrete products, stairs. Producers typically declare their dimensional tolerances against that standard and against the common rules in EN 13369, and many work to a minimum concrete class of C30/37 for stair elements. The exact tolerance and class belong in the project specification, not in a supplier's brochure.
Two ways to cast a flight
There are two established methods, and the choice drives tooling cost, surface quality and labour. The first is vertical or side casting in a dedicated stair mould, with the steps facing sideways. The flight stands on edge during casting and demoulding, so three faces come out of a steel mould: the two long sides and the soffit. A trade report on a Hungarian precast plant describes this arrangement in detail, with paired moulds taking 4 to 18 steps, widths from 800 to 1,600 mm, goings adjustable from 220 to 320 mm, risers from 150 to 200 mm and landings up to 400 mm. Riser and going adjustment is powered and synchronised, which is what makes a single mould cover a range of storey heights.
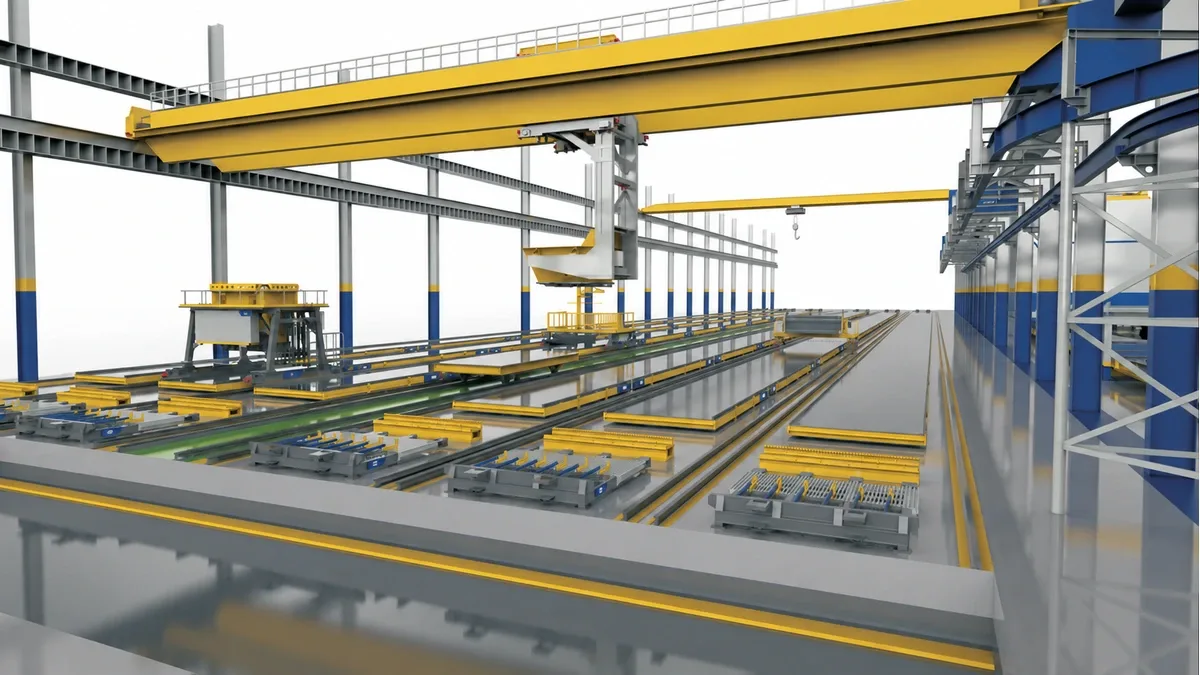
The second is flat casting on a tilting table or a casting pallet, with side shutters forming the steps and the top face finished by hand or by a powered trowel. Tooling is cheaper and the table can be reused for other components, but only the face against the table is a true mould face. The step nosings and the exposed side need finishing, and that labour is the hidden cost in this method. Stationary precast plant descriptions list both tilting tables and dedicated staircase moulds as standard equipment for the same factory, because most plants end up with both.
A mixed arrangement is common: vertical moulds for the repeated standard flight, flat casting for landings, balconies and the odd geometry that does not justify a mould.
Fixed or adjustable steps
An adjustable stair mould costs more than a fixed one and pays for itself when the project mix moves. The engineering question is what adjusts: the riser, the going, or both, and whether the adjustment is manual or powered.
Manual adjustment with spacers and bolted step plates is adequate when a mould changes setting between projects rather than between casts. It is slow, and every change is an opportunity for a setting error that shows up as a 3 mm step difference at handover.
Powered adjustment on a synchronised mechanism suits plants running several floor heights in the same week. It costs more per mould and needs maintenance on the actuators, and it moves setting time from an hour to minutes. Neither option is better in the abstract. The deciding figure is how many setting changes the mould will see in a year.
There is also the question of what the mould does not adjust. Waist thickness, flight width and the landing detail are usually built in, so a change in those means a new mould or a modified one. Buyers who expect their product range to widen should say so before the mould is designed, not after. The range of stair geometry a mould can cover is set at the drawing stage.
How many moulds the programme needs
Mould count follows from the delivery programme, not from the plant area. The arithmetic is short enough to do before the enquiry.
Take a 20 storey building with two flights per floor and one stair core: 40 flights. If the frame programme runs for 10 weeks, that is 50 working days, or 0.8 flights per day. One mould casting one flight per day covers the peak with slack, provided curing is accelerated enough for a daily turnover. Add a second mould when the building has two floor heights, or when the landings are cast in the same mould and the setting has to change mid programme.
Two corrections usually appear once the plant looks at the real programme. First, stair flights are needed early, because the stair core is what lets the trades move between floors, so the demand curve is front loaded rather than uniform. Second, the same mould has to serve more than one project at a time, which means the setting has to change without stopping the line. Both push the count up. The same logic applied to beam lines is worth reading alongside this one, because the constraint is always the same: the mould is the bottleneck, not the concrete.
Balconies on the same line
A balcony is a cantilever slab with an upstand, a drainage fall, often a thermal break and always a set of connection details at the slab edge. It casts flat, demoulds by tilting or by lifting, and stacks without much difficulty.
The reason to produce balconies on the same line as stairs is that they share the same finishing and storage resources and the same project timing. The reason to be careful is that a balcony is exposed on five faces, so the mould face and the edge detail decide the appearance of the finished building. A balcony mould with a rough edge upstand will be visible from the street for the life of the building.
Balcony slabs also carry the fixing for the balustrade, usually cast in as a plate or a sleeve. Position tolerance on those items is tighter than on the slab itself, because the balustrade is not adjustable on site.
Stripping, lifting and the road
Demoulding strength governs the daily cycle. A common producer rule is to strip when the concrete reaches at least 50 percent of its design compressive strength, unless the drawings say otherwise, which is why stair lines are usually paired with accelerated curing rather than relying on ambient conditions.
Lifting is the other constraint. A flight 1.2 m wide with a 3 m rise, a 180 mm waist and 17 steps of 167 mm by 280 mm has a concrete volume of roughly 1.7 cubic metres, or about 4.2 tonnes at normal weight. That is a two leg lift with a spreader, and it needs cast in or drilled lifting points positioned so the flight hangs at its installed angle rather than flat.
Road transport then sets the practical width. In China, a vehicle and load wider than 2.55 m, taller than 4 m or longer than 18.1 m falls under the oversize transport regulation and needs a permit, with escorts and route approval above 3.75 m width or 28 m length, according to the Ministry of Transport regulation. European limits sit at a similar 2.55 m. A 1.6 m wide flight travels without drama. A flight with a 2.5 m landing may not, and the answer is to cast the landing separately rather than to buy a permit for every load.
What to put in the enquiry
| Item | What to state |
|---|---|
| Product range | Flight widths, storey heights, riser and going ranges, landing sizes, balcony sizes |
| Casting method | Vertical mould, flat table or both, and which components go where |
| Adjustment | Which dimensions adjust, manual or powered, and how often the setting changes |
| Output | Flights per day at peak, and the front loaded demand in the first weeks |
| Finish | Which faces are mould faces, and the finish class for the others |
| Curing | Whether accelerated curing is in scope and how stripping strength is verified |
| Handling | Lifting points, stacking method, and the widest load that must leave the gate |
| Interfaces | Connection plates, balustrade fixings, drainage outlets and their tolerances |
A stair and balcony line is small compared with a beam factory, and most of its problems are small as well: a mould that cannot adjust to the next floor height, a stripping strength that arrives a day late, or a flight that will not pass through the site gate. Settling those points before the equipment package is planned as a production line is cheaper than settling them on site.