What an armour unit line produces
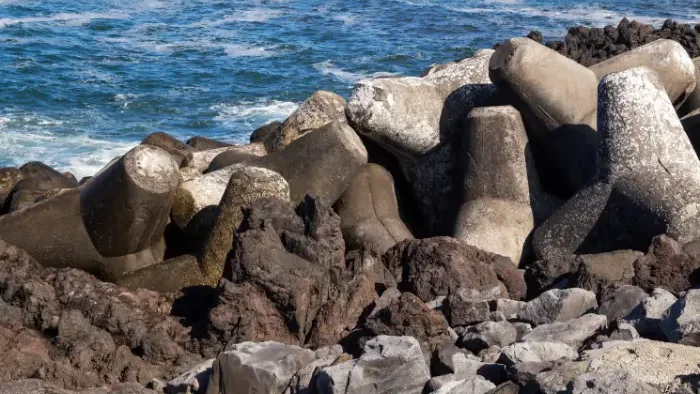
Armour units are the concrete elements placed on the outer layer of rubble mound breakwaters, revetments and similar coastal protection works. They are not structural building components. The design question they answer is hydraulic: how much mass, in what shape, holds its position against wave attack, and how the units interlock once placed.
The family is broad. Cubes are the simplest. Tetrapods and other multi-arm units rely on a shaped geometry. Single-layer interlocking units achieve stability with one unit layer instead of two, which changes the armour layer thickness and the number of units the project needs. The reference most designers work from is the Rock Manual, published by CIRIA as C683, which tabulates unit types against layer coefficients, packing densities and porosity so that armour layers can be compared. A summarised set of those parameters appears in published research on armour unit stability and structural response.
For the producer, all of this arrives as a bill of quantities: a number of units per type, a mass per unit, a total supply that has to be met to a programme. The production line is the answer to that bill.
Some single-layer units are protected designs. Where that applies, the approved geometry, the drawings and any proprietary name have to come from the client's documents, and a mould supplier should not be asked to reproduce a protected shape from a photograph.
Why unit mass drives the equipment list first
Mass is the first number to fix, because it sets everything downstream. Normal weight concrete runs at roughly 24 kN/m3, so a unit of three cubic metres is around seven tonnes before reinforcement and lifting gear are considered, and units in coastal works commonly reach tens of tonnes.
That figure decides the crane or wheel loader that strips and stacks the unit, the strength and flatness of the casting area, the size of the yard that has to hold the production of several weeks, and the transport method to the breakwater. Handling is not a side issue for these units either. Published stability research treats the ability of a unit to survive the stresses of handling as part of its structural performance, alongside wave loading, which is why the lifting point, the sling arrangement and the point of first lift are usually specified by the designer rather than improvised in the yard.
A line planned around small units cannot simply be scaled up. Doubling the unit mass roughly doubles the cast volume but changes the crane class, the mould mass, the stripping method and the yard circulation.
Moulds and the casting method
Armour units are cast in steel moulds, and there are two broad ways to get the unit out of the mould.
The first is a single-piece or open mould that is lifted off the unit. This works where the geometry has enough taper for the mould to release vertically, and it is the arrangement described in published practice for some repeating coastal unit families, where an open-ended mould with a taper is drawn upward off the cured unit by crane. It is fast and simple, and its limitation is geometry: shapes with re-entrant sections cannot be released this way.
The second is a segmented panel mould that is stripped around the unit. The Realjet tetrapod moulds page describes this arrangement, with steel panels built around the approved four-arm geometry, joint, locking and sealing details reviewed for repeated casting, and the opening sequence coordinated with the lifting and handling equipment available in the yard. Interlocking single-layer units normally fall into this group, because the interlock geometry is what the mould has to reproduce accurately if the armour layer is to behave as designed.
| Casting arrangement | Suits | What it demands |
|---|---|---|
| Open mould lifted off the unit | Geometric shapes with adequate taper and no re-entrant sections | Crane time on every unit, clear vertical access, stable unit support |
| Segmented panel mould stripped around the unit | Multi-arm and interlocking units with complex geometry | Panel mass and storage space, joint and sealing maintenance, defined opening sequence |
| Mould on a transfer or tilting arrangement | High unit counts on a fixed station | Rails or foundations, handling interfaces, layout space |
The marine and coastal moulds family shows how these mould systems are grouped for breakwater and coastal protection work.
Mould count before automation
Output planning for armour units is arithmetic, and it is worth doing before any conversation about automation. Each casting position is occupied for the whole cycle: filling, consolidation, the set period before stripping, stripping, and cleaning and preparing the mould for the next unit. If the cycle occupies a mould for two days and the programme needs forty units a day, the line needs at least eighty moulds, plus whatever buffer the producer wants for maintenance and for the days when curing runs slowly.
Two consequences follow. The first is that mould quantity, not mould sophistication, is usually the lever that sets output for this product family, and moulds are also a large share of the yard area because each one occupies floor space whether or not it is full. The second is that the arithmetic should be done with the real cycle time of the proposed mix and the real stripping rule, not with an average borrowed from another product.
Where a project needs a very large number of identical units, a circulating arrangement with dedicated positions can make sense. Where the project has several unit types in modest quantities, a batch of moulds served by one crane is usually the better fit, even though its peak output is lower. The same capacity logic, cycle time against installed output, applies to any line-based precast production.
Concrete, stripping and the first lift
Armour units are usually made from a mix designed for the exposure, and the yard has to place and consolidate it in a mould that may be more than two metres in any direction. Consolidation access matters more than it looks: internal vibration is impossible in most unit shapes once the mould is closed, so the mould arrangement, the placing sequence and any external vibration have to be planned together.
Stripping is governed by strength, not by the clock. The unit can be stripped and lifted once the concrete has reached the strength the project specifies for handling, and every hour saved before that point is taken from the margin. Where steam or another accelerated curing method is used to shorten the set, the cure has to suit the mix and be recorded, and the stripping decision still belongs to the strength result.
Form release, mould cleanliness and the condition of the panel joints also show up directly in the appearance of the units. Coastal units are not architectural work, but a mould that leaks at the joints produces fins and honeycomb that the client may reject on sight, and the sealing details in a segmented mould are maintained rather than ignored.
Storage, stacking and re-handling
A yard holding hundreds of units is a structural arrangement in itself. Units are heavy, they have an irregular shape, and they are stacked while the concrete is still young. Random stacking of irregular units is dangerous and wasteful; uniform stacking patterns use the available space and give a stable pile, which is the point the research linked above makes when it compares storage arrangements with placement on the slope.
Three questions are worth settling before the layout is drawn. How many units must be stored at once, which follows from the production rate and the transport programme to the breakwater. Whether the units are stacked in the orientation the designer intended, because point loads on a single arm can crack a unit in storage. And how the yard crane reaches the far side of the pile, because reach decides the pile height and the aisle width, which in turn decide the yard area.
Yard, plant and utility inputs
The site inputs for this line are dominated by unit mass and by the yard, and many of them are civil rather than mechanical:
- a casting area with hard standing designed for the unit mass and for repeated crane travel
- crane coverage over the casting positions, the stripping area and the whole storage pile
- a batching plant and admixture storage sized to the peak daily concrete volume
- water supply and washout provision, which is significant for textured units
- a cure method, whether ambient, steam or another accelerated route, with its energy supply
- access for the transport that removes finished units, including the route to the breakwater and any temporary works on it
That last item is often the constraint that governs everything else, because the transport of units of tens of tonnes to the works is a project in its own right.
What to settle before requesting a line
A supplier can scope a line properly once the enquiry carries the unit families with their masses and quantities, the approved geometry drawings, the programme and daily output required, the lifting point and sling arrangement, the stripping and handling rule, the curing method, the available yard dimensions and crane class, the transport method off site, and the acceptance standard the client intends to apply.
Where the unit families are still under hydraulic study, that is the right time to say so. A line quoted against a provisional unit family is a provisional line, and the mould count will move when the design is fixed.
Next step
Fix the unit families and their masses, then the daily output and the cycle time, then the yard and crane that go with them. Those three answers set the mould count, the casting arrangement and the plant, and they let two suppliers be compared on the same production brief rather than on two interpretations of capacity.
Realjet develops production lines for precast concrete components, including the mould systems, casting arrangements, curing provision and handling interfaces that go with them, and the coastal unit moulds described here sit within that scope. Final line configuration, equipment boundaries and acceptance criteria are confirmed in the approved project documents before manufacturing.