
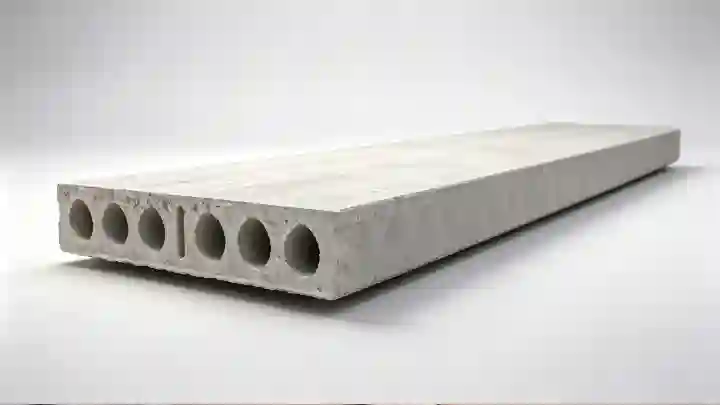
What a hollow core slab production line makes
A hollow core slab is a precast concrete floor or roof unit with continuous longitudinal voids. The voids cut self-weight and material use while keeping the slab strong enough for long spans and flat soffits. The production line makes these slabs as a continuous strip on a long casting bed, then cuts them to project length. The output is the slab itself; the line is the equipment, beds, prestressing and cutting systems that produce it.
Hollow core slabs suit residential and commercial floors, roofs, parking decks and industrial spans where a flat underside and fast installation matter.
Extrusion and slipform: the two casting methods
Two casting methods dominate. In the dry-cast or extrusion method, a very low-slump concrete is forced through a moving machine that shapes the slab and forms the voids with augers or cores. Extrusion is the global standard for hollow core because it gives high output, dense concrete and tight tolerances. In the wet-cast or slipform method, a higher-slump concrete is shaped by a machine that slips along the bed, with cores formed by tubes or fillers.
The machine is effectively the mould. It travels along rails on the casting bed, compacts the concrete, forms the voids and leaves a finished slab behind it. Because the slab is cast continuously, strand layout and slab thickness drive production efficiency more than individual piece count.
Consistent output depends on a stable low-slump mix, steady machine travel speed and accurate strand tension. Small variations in any of these show up as changes in slab density, void shape or soffit quality, so the line needs reliable concrete supply and machine control rather than manual adjustment during a cast.
From bed preparation to cut-to-length
A typical cycle starts with a long-line bed, often in the range of 90 to 180 metres, that is cleaned and prepared. High-tensile prestressing strands are laid along the bed and tensioned. The extruder or slipformer then casts the slab continuously while the strands are embedded. The slab cures on the bed, often with steam to reach early strength, and is cut to length with diamond saws once it is strong enough.
Prestressing is what lets the slabs span long distances. After cutting and release of the strands, compressive stress remains in the slab. Handling, storage and transport then follow, with care taken not to crack the slender units before they reach the site.
Capacity, beds and factory space
Installed capacity depends on bed length, number of beds, mix design, curing method and cutting rate, not on a single machine figure. A buyer should plan bed length and count around the typical slab thickness, span mix and daily or weekly output target. Because slabs are cut to length from a continuous cast, mixing projects with the same strand and thickness requirements on one bed improves efficiency.
Factory space must allow bed access for strand tensioning, concrete delivery, machine travel, cutting and lifting. Utilities include power for the machine and curing, water for concrete and curing, and steam generation where accelerated curing is used. The floor and roof slab moulds family shows how slab geometry and void layout are configured for different projects, which is a useful reference when defining slab types.
What buyers should define before purchase
Before approaching a supplier, define the slab range: thickness, width, typical spans and void layout. State the target output, the casting-bed length available, the curing method and the site conditions such as climate and utility limits. Prestressing strand layout, concrete mix permissions and any regional product standard, for example the PCI hollow core slab design manual in the United States or the European hollow core slab product standard, should be named so the equipment and process match the finished-slab requirements.
Also decide the level of automation and the handling plan. A continuous line needs coordinated concrete supply, machine control, cutting and lifting. The buyer's job is to package the product requirements, output target and site constraints so the supplier can propose a line that fits, rather than a generic machine list. End treatment, such as a cast-in topping or surface preparation for composite action with a screed, also belongs in the specification, because it changes the machine and the bed setup.
Where this line fits Realjet's production-line scope
Realjet supplies project-specific production lines for precast concrete components, including the engineering, equipment and, where confirmed, installation and commissioning scope. A hollow core slab line is one configuration within that range. Buyers evaluating such a line should start from the slab types, output target and factory conditions, then review the equipment package, utilities and responsibilities with the supplier before committing.
For slab-specific tooling and geometry, the precast concrete moulds range and the slab mould family give context on how formwork and void configuration are approached for precast floors and roofs.